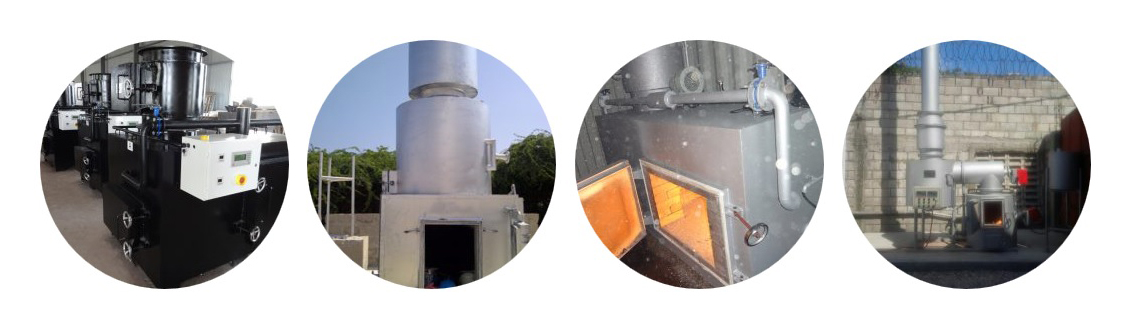
HICLOVER Waste Incinerators: Precision Engineering for Sustainable Waste Management
Introduction
In the world of waste management, the significance of waste incinerators cannot be overstated. These systems serve as critical tools for the effective disposal of hazardous materials, medical waste, and other refuse, all while adhering to stringent industrial standards. HICLOVER stands out as a leading manufacturer of hazardous waste incinerators in China, providing solutions that operate within the essential temperature ranges necessary for efficient combustion. With advanced engineering reliability and compliance with health standards, HICLOVER waste incinerators are designed to tackle the complexities of modern waste disposal.
Understanding Waste Incineration Technology
To comprehend the value of HICLOVER’s offerings, it is important to understand the technical underpinnings of waste incineration. Incineration is a thermal treatment process that reduces waste volume and hazardous characteristics through combustion. The technology is predicated upon effective temperature management, typically requiring operational temperatures between 850°C to 1200°C to ensure complete combustion and minimize toxic emissions. This is particularly vital for medical incinerator operating temperature standards to safely dispose of biomedical waste.
Combustion Principles and Regulatory Compliance
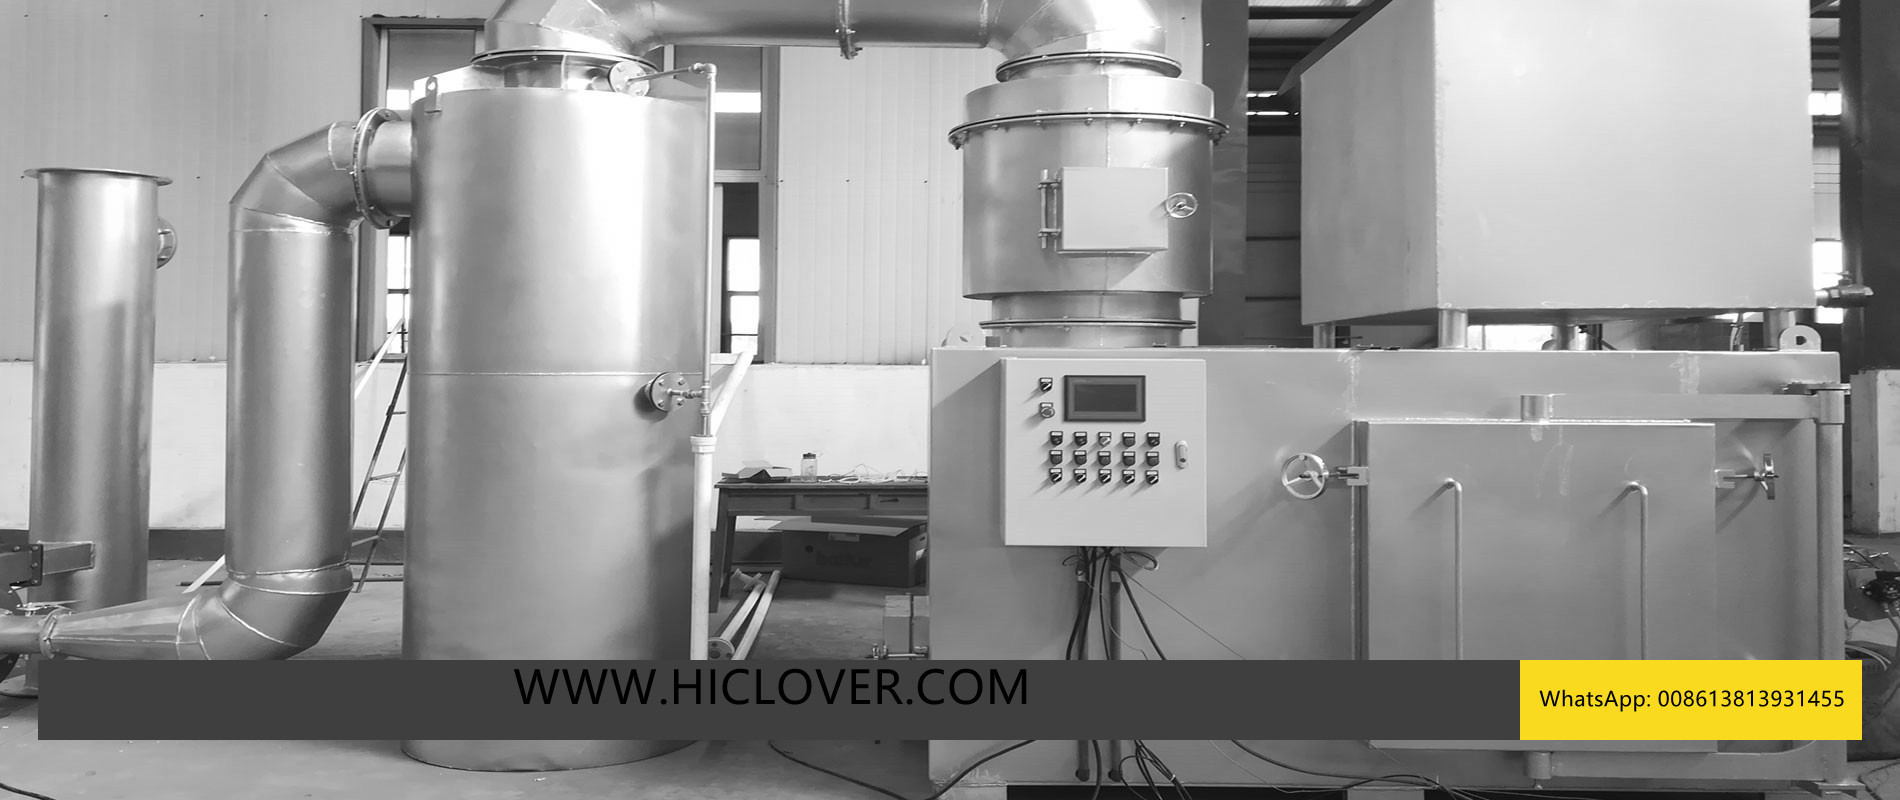
HICLOVER waste incinerators utilize dual combustion chambers to optimize combustion efficiency. The first chamber facilitates the primary burning of waste, while the second chamber ensures complete oxidation of any remaining flue gases, thereby enhancing safety and compliance with international regulations such as those set forth by the WHO and EU emission frameworks. Such designs not only meet but often exceed the regulatory requirements, making them suitable for various applications, from hospitals to industrial waste processing.
High Temperature Retention and Emission Control
High temperature retention is critical for ensuring that harmful byproducts are eliminated during the incineration process. HICLOVER’s systems are equipped with advanced thermal insulation and control technologies that allow for consistent high-temperature operation. Furthermore, the choice between wet and dry scrubbers enables clients to customize their systems to meet specific emission control goals, thus supporting their environmental, social, and governance (ESG) compliance objectives. The integration of such technologies positions HICLOVER as a leader in sustainable waste management solutions.
Commercial Investigation: Exploring Incinerator Types
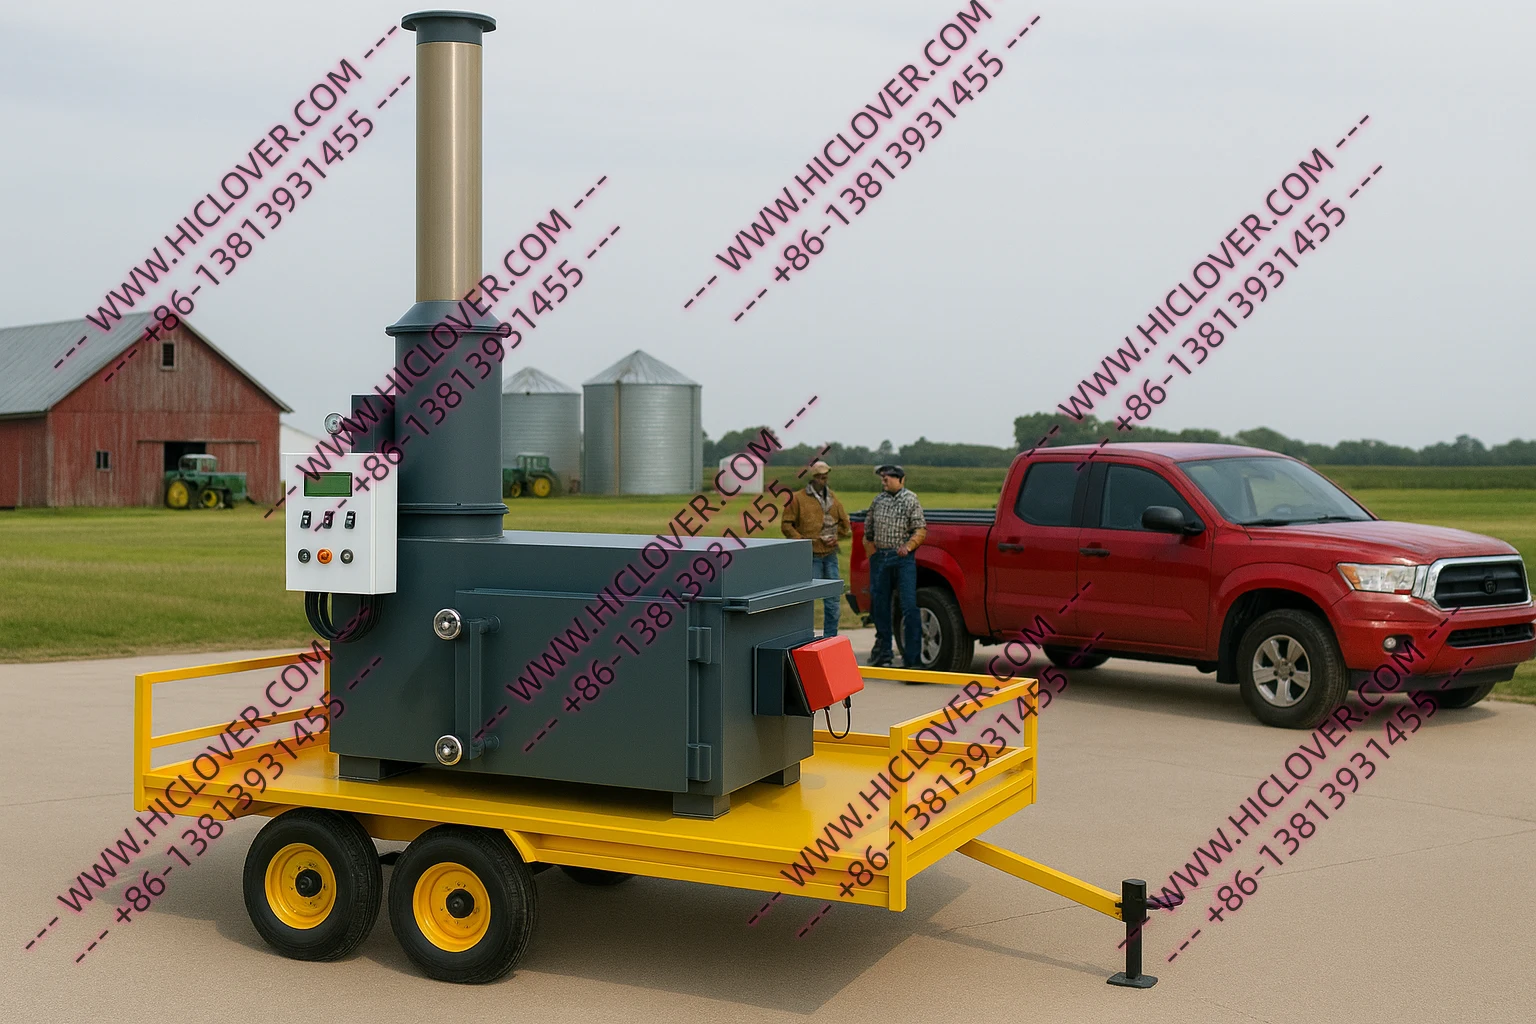
When evaluating waste incinerators, procurement managers must consider various types, including fixed and containerized models. Fixed systems are typically designed for large-scale operations, providing high throughput. In contrast, containerized systems offer flexibility and are particularly suited for remote site applications, such as in crisis zones and humanitarian camps. HICLOVER specializes in both types, leveraging its engineering expertise to deliver tailor-made solutions that meet diverse operational needs.
Control Systems: PLC vs. Manual
The control system is another key aspect in selecting an incinerator. HICLOVER incorporates programmable logic controller (PLC) automation into its designs, offering sophisticated monitoring and operational capabilities. This automation enhances operational efficiency and safety, enabling remote management and real-time data collection—a critical feature for industries focused on reducing operational costs while ensuring compliance. Manual controls may still be favored in some scenarios; however, as industries increasingly embrace digital automation, PLC systems are becoming the preferred choice for their reliability and performance.
Scrubbing Technology: Dry vs. Wet
HICLOVER offers both dry and wet scrubbing systems, providing clients with the ability to tailor their waste management solutions based on specific emission needs and site conditions. Dry scrubbers are known for their reduced water consumption, while wet scrubbers are effective in capturing fine particulate matter and acid gases. The ability to select between these systems allows for a customizable approach that aligns with the client’s operational goals, making HICLOVER’s solutions highly competitive in the global market.
Transactional Insights: HICLOVER’s Market Value
One of the significant advantages of partnering with HICLOVER is the factory-direct supply model. Unlike trading companies, HICLOVER manufactures its systems in-house, ensuring stringent quality control processes and a stable supply chain. This direct access to factory pricing translates to cost savings for clients, making it an economical choice for procurement managers. Furthermore, the capacity for customization allows HICLOVER to cater to specific chamber volume requirements, thus optimizing operational efficiency based on waste types.
Global Export Capability and Engineering Experience
With a robust global export capability, HICLOVER services clients across various markets, including regions such as Seychelles and Libya, where Seychelles animal incinerator prices and Libya pet incinerators are of significant interest. HICLOVER’s engineering experience translates into reliable, high-quality equipment that is engineered to withstand the rigors of diverse operational environments, including decentralized waste management systems in remote mining or oil camps.
Customized Solutions for Diverse Applications
The modular design of HICLOVER’s waste incinerators, particularly the mobile plug-and-play systems, allows for rapid deployment in various settings. This feature is increasingly relevant in today’s world, where the demand for emergency response capabilities is rising due to global infectious disease preparedness and environmental crises. By utilizing versatile designs, HICLOVER can meet the needs of a rapidly changing market, ensuring clients can handle waste efficiently while adhering to local regulations.
Conclusion
HICLOVER stands at the forefront of the waste management industry, offering advanced waste incinerators that are engineered for reliability, efficiency, and compliance. With a firm commitment to sustainability and innovation, HICLOVER not only meets the demands of today’s waste management challenges but also positions itself as a trusted partner for procurement managers and decision-makers across the globe. The company’s focus on high standards, combined with competitive pricing and customizable solutions, makes HICLOVER a pivotal asset in the quest for effective waste disposal.
For more detailed information on HICLOVER and their innovative waste incineration solutions, visit HICLOVER’s website.